1-805-484-2992
Quotes - Engineering - SalesThe construction for product that will not go through a plate
A sanitary tube-in-tube exchanger runs the product through an inner tube and the utility through the annulus between that tube and an outer jacket. There are no baffles, no gaskets in the product path and no channel narrower than the product tube itself, so anything that fits through the inlet ferrule passes the exchanger. Modules are built in straight lengths and joined with sanitary return bends into a hairpin or serpentine bank, giving pure counterflow and a temperature cross that a single-shell exchanger cannot manage. Pressure capability runs to several hundred psi on the product side because the tube is a simple cylinder, and temperature is limited only by the gasket at the return bend.
Product tube
- 1" to 4" OD, single or multi-tube bundle
- Smooth or corrugated wall, 32 Ra or better inside
- Tri-clamp inlet and outlet, sized to the largest particle
- Removable inner tube on single-tube modules
- Straight bores, pig and brush cleanable
Jacket and utility
- Annulus sized for 3 to 6 ft/s utility velocity
- Steam, hot water, chilled water or glycol
- Counterflow through every module
- Tri-clamp, flange or NPT jacket connections
- Modules stacked on a stainless frame with return bends
Ratings and codes
- 150 psig standard, several hundred psi available on the product tube
- Design temperature to 350 F and higher
- ASME U-stamp on the jacket as required
- 3-A conformance where specified
- PED, CRN on request
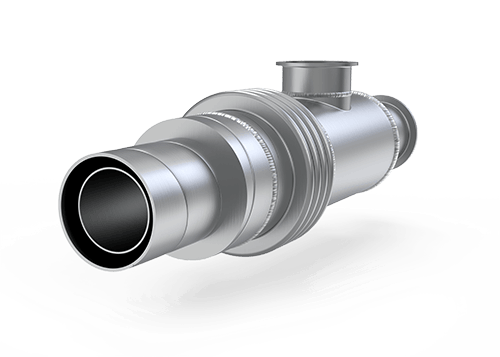
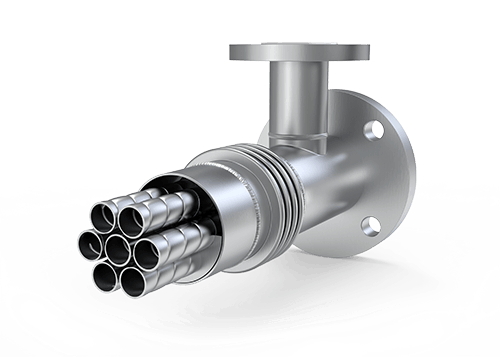
Talk to an Application SpecialistNothing in the product path is narrower than the tube itself, so whatever passes the inlet ferrule passes the exchanger in true counterflow.
Sized on product velocity: 2 to 3 ft/s minimum keeps solids suspended.
When tube-in-tube is the right sanitary answer, and how it is sized
Viscosity, particulates and the plate boundary
Plates run out of room in two directions. Above roughly 500 cP the pressure drop through a plate channel grows faster than the heat transfer, and above a particle size of about 1/8" on chevron plates or 3/8" on wide-gap plates the pack plugs. Tube-in-tube has neither limit in practice: a 1-1/2" product tube passes diced vegetables, whole berries, pasta, rice and meat pieces, and a 2" to 4" tube passes whole fruit. Viscous products such as purees, pastes, ketchup, honey, cream cheese and yogurt with fruit are pumped through at whatever velocity the pump can supply, and the exchanger is sized to the actual coefficient at that velocity rather than to a plate assumption.
Counterflow, temperature cross and gentle heating
Because each module is a single pass in one direction and the modules are connected in series, the whole bank is in true counterflow. The product outlet can be brought above the utility outlet, a temperature cross that a single-shell exchanger cannot do, and the approach at the hot end can be a few degrees. Sensitive products also benefit from the modest wall temperature difference that counterflow allows: the utility is only as hot as the local product needs, which keeps proteins from denaturing on the wall and keeps fruit from cooking at the surface.
- True counterflow through the entire bank
- Temperature cross available
- Wall temperature held close to product temperature
- Holding tube length added between banks for pasteurization
Sizing to velocity and shear
The number that governs a tube-in-tube design is product velocity. Viscous product in a smooth tube is laminar, and the coefficient in laminar flow depends on velocity and tube length in a way that rewards long, narrow tubes up to the pressure the pump can deliver. Particulate product has a different constraint: velocity high enough to keep solids suspended, generally 2 to 3 ft/s minimum, and low enough that shear does not damage the pieces. The sizing balances tube diameter, bank length and pressure drop against those limits, and the corrugated tube option is brought in when the laminar coefficient is to low for a practical length.
Drainability, cleaning and thermal growth
The bank is mounted with each module pitched toward its outlet and the return bends at the low points fitted with drains, so the product path empties by gravity. CIP is run through the product tube at pigging or brush velocity, and single-tube modules allow the inner tube to be withdrawn for inspection. On the utility side the annulus drains at the jacket connections. Because the inner tube and jacket run at different temperatures, one end of each module is free to move, either with a sanitary gland or an expansion element on the jacket, and that detail is what keeps a steam-heated bank from working the welds loose over a season.
For product that plates cannot pass and shells cannot keep clean, tube-in-tube is the construction that makes the process simple.
Call and talk it through with an engineer: 1-805-484-2992
Choosing the Build
Start with the largest piece, then the viscosity, then the length the bank would need. Whole fruit, diced vegetables and meat in sauce need the single tube's open bore, sized so the largest piece is about one-third of the bore. Pulp, seeds and fibers that pass a 3/4 inch to 1-1/2 inch tube point to multi-tube, which puts several times the surface in each foot of frame. Then look at the laminar coefficient: a smooth tube in laminar flow gains only about 26 percent in coefficient when velocity doubles, so if the bank runs too long, corrugation is added to whichever tube type the pieces allow. Send particle size, viscosity hot and cold, and flow; those three settle it.
Yes, by running product in both the inner tube and the annulus, or more often through a closed water loop between the hot and cold banks. Product-to-product puts product in the annulus, which then has to be polished, drainable and cleaned at velocity around spacers and jacket welds; it is done, but it limits the design. Indirect regeneration circulates water from the outgoing product's jacket to the incoming product's jacket, costs a pump and some approach temperature, and keeps both product paths standard. On a particulate line recovering 50 to 60 percent of the heat this way is realistic; the 85 to 90 percent a plate pack reaches is not.
Modules run 10 to 20 feet long and stack vertically on a frame, so a 400 foot bank is twenty 20 foot modules in a frame roughly 8 to 10 feet tall and 22 feet long. The frame needs clearance at one end to withdraw inner tubes on single-tube modules, headroom for the return bends at the top, and a floor drain at the low end where the bank empties. Give us the room's length, height and door size with the inquiry, because splitting a bank into two frames or shortening modules is easy on the drawing and expensive afterward.
Related
Sanitary Exchangers
Shell & Tube
Straight tube, U-tube and double tubesheet bundles built for steam, pressure and a clean CIP return.
+ Learn More
Sanitary Exchangers
Plate & Frame
Close approach, regeneration and a pack that opens for inspection: the pasteurizer's construction.
+ Learn More
Sanitary Exchangers
Embossed Plate
Two stainless sheets welded and inflated into a heat transfer surface that goes wherever the tank needs it.
+ Learn More