1-805-484-2992
Quotes - Engineering - SalesThe heater on the CIP skid
Every clean-in-place system in a sanitary plant has at least one heat exchanger in it, and it is the one that sets the cycle time. A typical program is a pre-rinse with warm recovered water at 100 to 140 F, a caustic wash with 1 to 2 percent sodium hydroxide at 160 to 180 F for 20 to 40 minutes, an intermediate rinse, an acid wash with 0.5 to 1 percent nitric or phosphoric acid at 140 to 160 F for 10 to 20 minutes for milkstone and mineral scale, a final rinse and a sanitizer. The CIP supply heater has to lift the solution to those temperatures either in the tank before the cycle or in line as the solution goes out, and it has to do it at the CIP flow rate, which is set by the requirement for 5 ft/s in the largest pipe on the circuit and is usually higher than the process flow.
The heater is almost always a steam-to-solution shell-and-tube: plant steam on one side, CIP solution on the other, with a modulating steam valve controlled on the supply temperature. It is a utility exchanger by function but its solution side shares piping with the product path and is inspected as sanitary equipment, so it is built drainable, in stainless with a 32 Ra finish, with tri-clamp connections and a gasket compound that survives caustic, acid and the sanitizer.
Request a Quote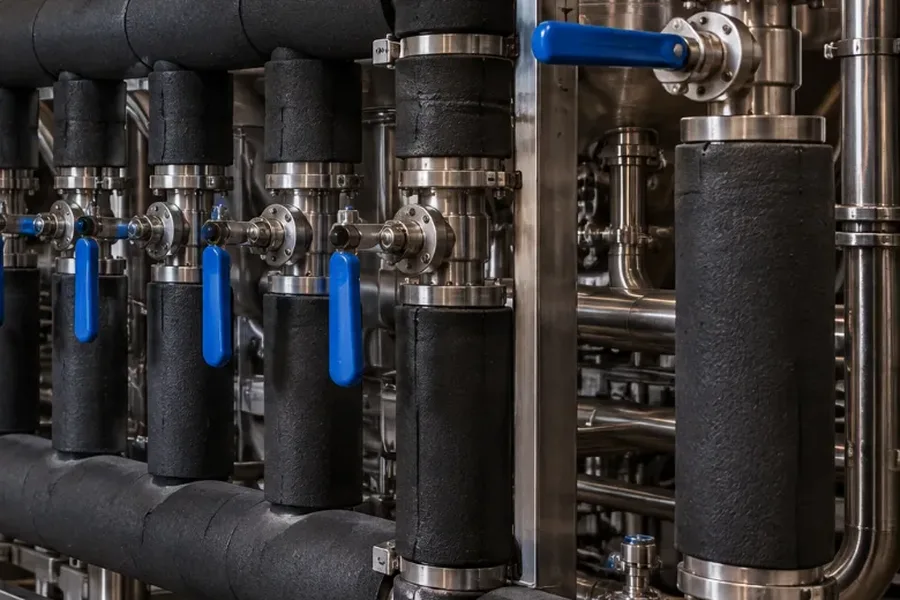
A 1,000 gallon tank from 120 to 170°F in 20 minutes
That is about 1.25 million Btu/h and 1,300 lb/h of steam; given an hour, the heater is a third the size. In-line heating at 200 gpm with a 50 degree rise is 5 million Btu/h, and the solution side is rated past the 150 psi shutoff head.
In-line CIP supply heater
- Heats solution in a single pass at the full CIP flow rate
- Steam on the tube side, solution on the shell side
- Modulating valve on supply temperature, 2 to 3 degree control
- 304 or 316L solution side, EPDM seals
- Sized on flow and rise, not tank volume
Tank heating and rinse recovery
- Recirculation heater lifts the tank in 15 to 30 minutes
- Sized on tank volume, rise and the time the cycle allows
- Rinse recovery exchanger reclaims heat from final rinse to pre-rinse
- Vented and drained so caustic does not sit in the shell
- Design pressure covers the CIP pump shutoff head
Recommended construction by CIP duty
CIP heaters are steam-to-liquid duties on a corrosive but non-fouling fluid. The geometry follows the steam and the cleaning of the heater itself.
| DUTY / CONDITION | RECOMMENDED CONSTRUCTION | WHY |
| In-line caustic and acid supply heater on plant steam, 50 to 500 gpm | U-Tube | Steam on the tube side with free expansion; solution on the shell at low pressure drop; bundle pulls for inspection |
| Recirculation heater on a CIP tank, batch heat-up in 15 to 30 minutes | Straight Tube | Fully drainable so caustic never sits; brushable; steam or hot water on the shell side |
| Single-pass CIP for a small plant or a mobile CIP cart | Gasketed Plate | Compact steam-to-water or hot-water-to-solution plate; opens for gasket change after years of caustic |
| Rinse water recovery, final rinse to pre-rinse | Gasketed Plate | Water-to-water at close approach recovers most of the final rinse heat; cheapest area for the duty |
| CIP solution heater where steam cannot enter the sanitary area | Clean Steam Generator | Clean steam made from RO or softened water heats the solution with no boiler chemicals near the product path |
| CIP heater on a line that is also steamed in place | Double Tubesheet | Where the same heater sees product-side steam at 250 F and plant steam on the utility side, the gap keeps them apart |
Sizing and building a CIP supply heater
The sizing question on a CIP heater is time, not duty. A 1,000 gallon caustic tank held at 120 F between cycles has to be at 170 F when the wash starts; if the schedule gives 20 minutes, the heater has to deliver about 1.25 million Btu/h, which is roughly 1,300 lb/h of steam and a heater with a 2 inch steam valve. If the schedule gives an hour, the heater is a third of that. In-line heating is sized differently: the solution goes out at the CIP flow rate, say 200 gpm, and must rise from the tank temperature to 170 F in one pass, which at a 50 degree rise is 5 million Btu/h and a much larger heater that runs only while the wash is out. Most skids do both: a recirculation heater holds the tank near temperature and the in-line heater trims.
Materials follow the chemistry. Sodium hydroxide at 2 percent and 180 F is not corrosive to 304 or 316, but the acid step, particularly nitric at 160 F, and the chlorine-based sanitizers some plants still use, argue for 316L on the solution side. Gaskets and seals are EPDM, which handles caustic, nitric and phosphoric acid and peracetic sanitizer; nitrile and silicone do not last. The heater is fully drainable so that caustic does not sit in a tube between cycles and concentrate as the water evaporates, and it is vented at the high point so it does not airlock on the first fill.
The design pressure of the solution side deserves a look. CIP pumps are chosen for head, because 5 ft/s through a long circuit with a spray ball at the end takes 60 to 100 psi at the pump, and the shutoff head can exceed 150 psi. A heater rated 100 psig on the solution side is a relief valve problem waiting to happen; HeatX rates the solution side for the pump's shutoff head and states the number on the drawing.
Sized on the cycle clock, built for 2 percent caustic
Heat recovery on CIP
A CIP cycle sends thousands of gallons of 170 F caustic and 150 F acid back to the tanks and thousands more of warm rinse to drain. A plate exchanger between the final rinse leaving the circuit and the fresh water filling the pre-rinse tank recovers 60 to 70 percent of that rinse heat, and a plant running ten cycles a day pays for the exchanger in a few months. The solution tanks themselves are kept warm between cycles by the recirculation heater at low fire rather than reheated from cold.
Heating the exchanger being cleaned
The heat exchanger on the process line is itself a CIP target. To clean a plate pasteurizer or a tube-in-tube, the CIP flow must reach 1.5 times the product flow so velocity in the largest channel passes 5 ft/s, and the caustic must arrive at temperature. A CIP supply heater sized on the process flow will fail that test; size it on the CIP flow the largest circuit demands.
Single-use and recirculating CIP
Single-use CIP makes fresh solution each cycle and sends it to drain, which suits small plants and allergen changeovers; the heater is in-line and sized for the full rise. Recirculating CIP reuses caustic and acid for weeks with make-up and filtration, and the heater is mostly a tank heater holding temperature. HeatX asks which type the skid is before sizing, because the heaters are different by a factor of three.
What to send for a quote
CIP flow rate, tank volumes, solution temperatures and the time allowed to reach them, steam pressure at the skid, chemistry including sanitizer, in-line or tank heating, and the CIP pump's shutoff head. Those numbers turn into a heater size and a steam valve size in one pass.
Call and talk it through with an engineer: 1-805-484-2992
Specifying the CIP Heater
Hold the tank warm and trim in line; pick one only when the skid forces it. A tank held at 140 F between circuits cuts the in-line duty from the full 50 degree rise to a 30 degree trim: at 200 gpm that is 3 million Btu/h instead of 5 million, and the steam valve drops a size with it. Tank-only heating suits a recirculating skid with 20 minutes or more between circuits; in-line-only heating is forced on single-use skids and one-pass dosing systems, where there is no warm solution to start from. The sign that a plant chose wrong is the first circuit of the shift running two or three minutes over because supply temperature is still climbing while the timer is already counting. Tell us the circuit sequence and the gap between circuits and we size both heaters, or confirm that one is enough.
Yes for rinses and the acid step; for 170 F caustic it works only with a much larger exchanger. A 190 F hot water supply cooled to 150 F against solution rising from 120 to 170 F gives a log mean temperature difference near 25 degrees; 15 psig steam at 250 F gives about 100 on the same duty, so the hot water heater needs roughly four times the area to match the ramp. A gasketed plate keeps that area affordable. The failure mode is a loop whose supply sags to 175 F when the pasteurizer draws, leaving caustic parked at 165 F with nowhere to go. Send the loop's supply temperature at its worst hour, not its setpoint.
Peroxide-cured EPDM, and the cure matters as much as the polymer. Sulfur-cured EPDM hardens and cracks sooner under repeated hot caustic, while FKM, the usual choice for acids, swells and loses strength in 2 percent sodium hydroxide at 170 F. On a U-tube heater the compound sits only in the head gasket; on a gasketed plate it lines every channel, so a plate on a full CIP program is bought with a spare gasket set and a replacement interval in mind. Chlorinated alkaline cleaners and any solvent flush move the choice toward PTFE-envelope gaskets. List every chemical in the program, including the one used twice a year.
Control on the heater outlet; verify on the return. The outlet RTD runs the steam valve because it sees the result of a valve move in seconds, while a return RTD sees it only after the solution has traveled the whole circuit, and a loop closed on that delay hunts for the entire wash. The return RTD is the one the cleaning record keeps, so the supply setpoint is carried 5 to 10 degrees above the required return temperature to cover loss along uninsulated pipe and through the equipment being cleaned. One RTD doing both jobs on the supply line proves only that the heater worked, not that the spray ball saw 170 F.
It takes a quarter of a 150 hp boiler the instant the valve opens. A 150 hp boiler makes about 5,175 lb/h, and the 1,300 lb/h a 20 minute heat-up demands arrives as a step, so header pressure drops and the HTST or evaporator on the same main sees its own steam valve swing wide. Three fixes: hold the tank warm with the small recirculation heater so the step shrinks, stagger CIP starts against production draws, and ramp the valve open over a minute or two in the sequence. Give us the header pressure at the skid under full production load.
No. Peracetic and most no-rinse sanitizers are dosed at ambient, and heating them speeds decomposition and attacks the seals. The practical issue is the heater's own heat: the shell of a 170 F caustic heater and the solution left in it keep the first sanitizer through at well above label temperature unless the sequence closes the steam valve and runs the final rinse long enough to cool the metal. A hot water sanitize step is the exception and is quoted as a separate duty with its own temperature and hold.
Related
Applications
High-Purity Water
RO, DI and demineralized water heated, cooled and tempered in metal that the water cannot take with it.
+ Learn More
Applications
Clean Steam & Aseptic
Clean steam from purified water for SIP and sterile barriers, and exchangers built to be sterilized and held.
+ Learn More
Applications
Water & Utility
The exchangers behind the process: high-purity water, CIP supply, clean steam and aseptic sterile barriers.
+ Learn More