1-805-484-2992
Quotes - Engineering - SalesThe workhorse for pressure, steam and long service
A sanitary shell and tube exchanger puts the product inside polished tubes and the utility in the shell around them. Because the product side is a set of smooth, straight or gently bent tubes with no gaskets between passes, it stands up to steam, high differential pressure and years of CIP without the periodic re-gasketing a plate pack needs. Typical units run 3" to 48" in shell diameter and 12" to 400" long, with tubes from 3/4" to 1-1/2" OD on a triangular or square pitch.
Product side
- 3/4", 1" or 1-1/2" OD tubes, 16 to 18 gauge
- Internal finish 32 Ra standard, 20 Ra or electropolished on request
- Channel heads machined from solid bar or plate, no crevice corners
- Tri-clamp or ASME BPE connections, 1" through 6"
- Orbital TIG seal welded tube-to-tubesheet joints
Utility side
- Steam to 150 psig, hot water, chilled water or glycol
- Segmental baffles at a spacing set for velocity, not just support
- Shell finish 40 Ra exterior, bead blast or polished
- Tri-clamp, ASME flange or NPT shell connections
- Expansion bellows for large temperature swing on straight-tube units
Codes and testing
- ASME Section VIII Div 1 U-stamp and National Board number
- 3-A 12-08 conformance where specified
- TEMA C for sanitary, B or R for heavier process service
- PED or CRN for export and Canadian installs
- Hydrotest, dye penetrant and profilometer readings on record
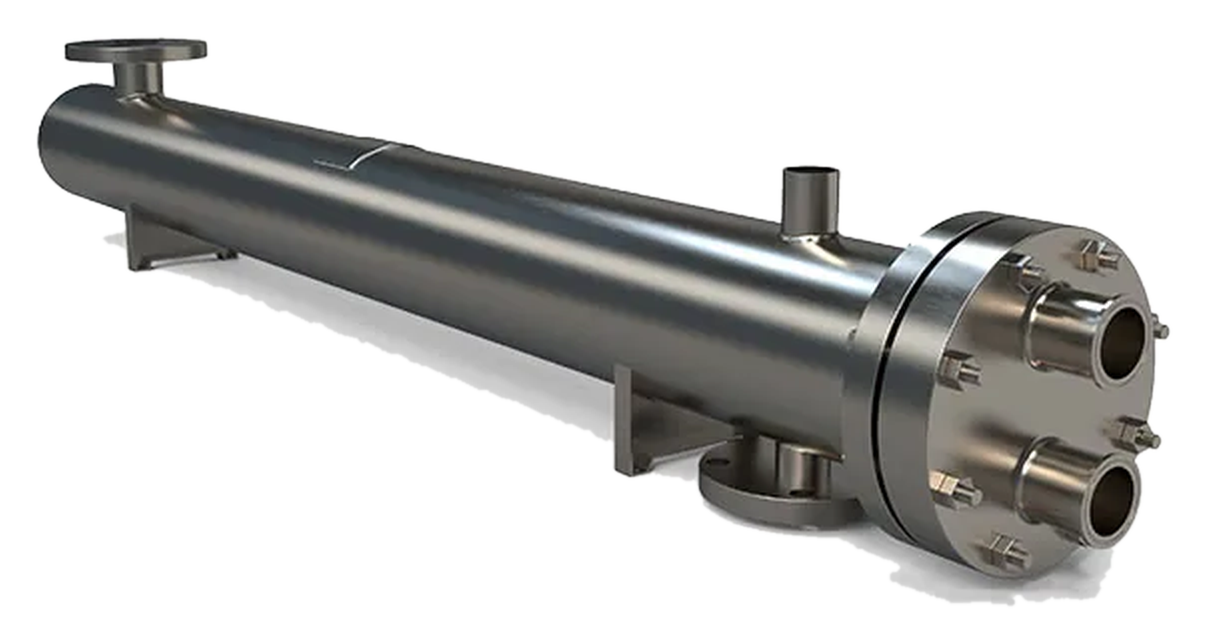
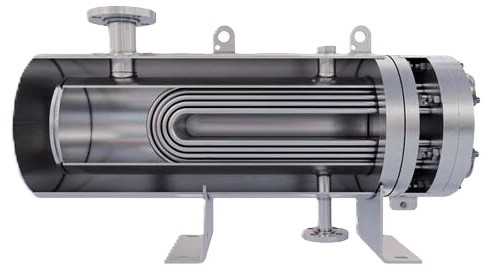
Talk to an Application SpecialistProduct runs inside seal-welded polished tubes, so steam, 150 psig and years of CIP never meet a gasket or a rolled joint.
Pick tube OD for the product, 4 to 8 ft/s for cleaning.
Designing a sanitary shell and tube for the duty in front of it
Tube size follows the product, not the catalog
The first number fixed on a sanitary shell and tube job is the tube OD, and it is chosen from what flows through it. Clear liquids and water-like products run in 3/4" tubes, which give the most surface per shell diameter and the highest tube-side velocity for a given flow. Products with small particulates, light pulp or a tendency to foul move up to 1" tubes. Anything with soft solids, or that must be brushed between runs, goes to 1-1/2". Wall thickness is usually 16 or 18 gauge; thicker walls only cost heat transfer and add nothing to a 150 psig design.
Velocity, fouling and the CIP return
Tube-side velocity is the second decision. Between 4 and 8 ft/s keeps most food products turbulent enough to scrub the wall and keeps CIP effective; below about 3 ft/s a milk or juice unit will foul early and the cleaning cycle will not reach the back of the fouling layer. Passes are added until the velocity lands in range, with the trade-off that each added pass raises product-side pressure drop. On the shell side the same thinking sets baffle spacing so the utility actually crosses the bundle instead of short-circuiting along it.
CIP is normally run at 160 to 180 F with caustic and acid cycles, and the design velocity in CIP mode should be at least 5 ft/s in every tube. A shell and tube unit sized on product flow alone can have tubes near the outer rows that see less CIP velocity; a good design checks both cases.
Joints, heads and where the crevices hide
Rolled tube joints are the classic sanitary failure: the tube-to-tubesheet gap traps product and is unreachable by CIP. On the product side every tube is seal welded to the tubesheet, usually by orbital TIG for repeatability, and the weld is ground and polished flush. Channel heads are machined from a single piece so there is no inside corner weld; the head-to-tubesheet joint is a tri-clamp or a sanitary flange with a food-grade gasket rather than a raised-face bolted joint.
Where product runs on the shell side instead, which is common for viscous product heated with hot water in the tubes, the shell interior is polished and the baffles are cut and pitched so the shell drains through a low-point outlet. That configuration is rarer and needs a longer conversation about baffle design.
- Orbital TIG seal weld on every product-side tube joint
- Heads machined from solid, polished to the tube finish
- Tri-clamp or sanitary flange head closure, no raised-face bolting
- Low-point drains on both sides in the installed orientation
Materials, finish and what is on the record
304L is standard for food and dairy; 316L is standard for pharma and for any product carrying chlorides, brine or acidified sauces. Tubes are seamless or welded-and-drawn with the weld bead removed so the internal finish holds 32 Ra or better across the full length. The unit is passivated after fabrication and electropolished if the spec calls for 20 Ra or lower. Material test reports, weld maps, hydrotest and profilometer readings ship with the unit so the validation package writes itself.
A sanitary shell and tube unit that is sized to the actual flow, tubed for the actual product and welded rather than rolled will run for decades.
Call and talk it through with an engineer: 1-805-484-2992
Standard steam-to-water units and spare bundles
Two cataloged ranges sit under this section for the buyer who needs a stock unit rather than an engineered one. The steam-to-water units are 6" and 8" sanitary shell and tube heaters in 304 or 316 stainless with tri-clamp process connections, rated 150 PSI and 375°F, in 54" to 96" tube lengths. The matching replacement tube bundles drop into those shells when a bundle has fouled or been damaged, so the shell, heads and piping stay in place. Each part number has its own page with the connection sizes, surface area and ratings.
Construction Questions
A straight tube unit with a shell bellows, or a straight tube heated by a hot water set rather than live steam. The two wishes pull against each other: U-tube takes the steam start-up without stress but hides its bends from a brush, while straight tube brushes end to end but locks tubes and shell together. Plant steam at 100 psig sits near 338 F; against a 40 F product start the metal differential far exceeds the 100 to 150 F a fixed tubesheet tolerates, so the bellows is doing real work. A hot water set holding the shell at 190 F cuts that differential to a level the fixed design handles alone, and it is gentler on burn-on. Choosing U-tube and hoping CIP keeps up with a product known to bake on is the choice that disappoints.
Mechanical details only: tolerances, baffle and tie-rod construction, minimum thicknesses and nozzle loads; nothing about finish, drainability or crevices. That is why a TEMA C sanitary unit and a TEMA R refinery unit can look alike on the data sheet and be entirely different inside. Class C suits the moderate duty most food and dairy units see; B adds requirements written for chemical plants and R for petroleum service, and either raises cost without adding one point of cleanability. Write TEMA C for the mechanical side and 3-A 12-08 or ASME BPE for the product side, and state both on the request.
Yes, but it is rarely the economical way. Both sides become product contact, so the shell interior must be polished, the baffles cut for drainage and the shell CIP cleaned at velocity, which is a longer conversation than a standard build. The bigger issue is the temperature cross. A plate pack recovers 85 to 90 percent of a pasteurizer's heat in one frame because its channels are true counterflow; a shell and tube with baffled cross flow needs two or three shells in series to approach the same recovery. Where regeneration is wanted on a product plates can not pass, a tube-in-tube bank in series gives the counterflow without the shell-side cleaning problem.
Work it from flow per tube: a 3/4 inch 16 gauge tube carries about 4.7 gpm at 5 ft/s, a 1 inch tube about 9.3 gpm. So 100 gpm of CIP solution through 3/4 inch tubes wants no more than 21 tubes per pass; if the thermal duty needs 84 tubes, that is a four-pass bundle. Run the same arithmetic for production flow, because a milk duty at 60 gpm through those 21 tubes is only 3 ft/s and will foul early. When the two flows disagree, the usual answer is to size passes for production at 4 to 8 ft/s and raise CIP flow to match, so tell us the CIP pump's capacity along with the product flow.
When the product is clean water or behaves like it, steam is the heating medium, and no special finish, second tubesheet or pharma documentation is required. The cataloged 6 inch and 8 inch units are rated 150 psi and 375 F in 54 to 96 inch lengths with tri-clamp process connections, which covers CIP solution heating, hot water sets, rinse water and sanitizing loops at a fixed drawing and a stock replacement bundle. Anything that fouls, carries solids, needs 20 Ra or a double tubesheet, or must cross temperatures in regeneration goes to an engineered unit.
Related
Sanitary Exchangers
Plate & Frame
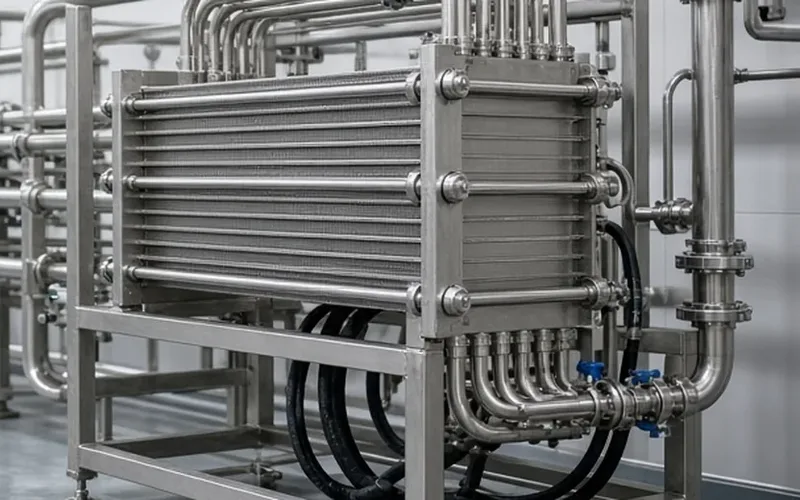
Close approach, regeneration and a pack that opens for inspection: the pasteurizer's construction.
+ Learn More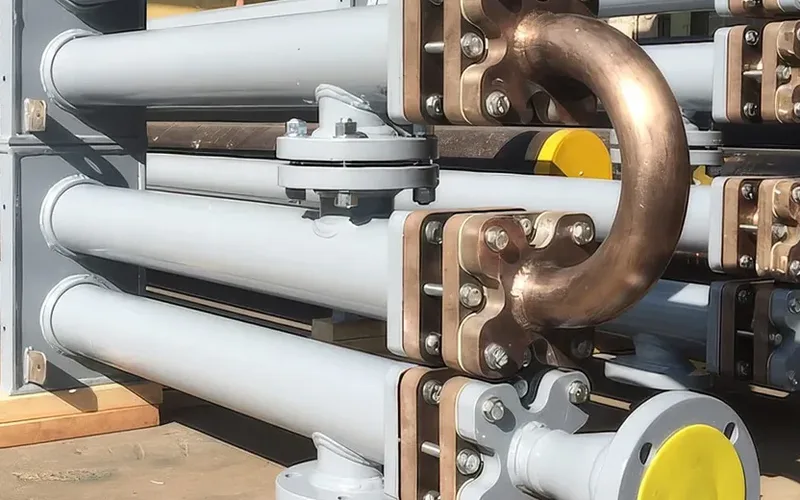
Sanitary Exchangers
Tube-in-Tube
One straight product tube inside a jacket: nothing to plug, nothing to bridge, and full counterflow.
+ Learn More
Sanitary Exchangers
Embossed Plate
Two stainless sheets welded and inflated into a heat transfer surface that goes wherever the tank needs it.
+ Learn More