
1-805-484-2992
Quotes - Engineering - SalesPaper is part of the product
A sanitary heat exchanger built for an audited plant is not complete when it passes hydrotest. It is complete when the documents that prove its materials, welds, finish and test results are assembled, cross-referenced and handed over. For a food plant that may be a few pages: mill certificates for the wetted metal, the gasket compliance statement, the hydrotest report and the drawing. For a pharmaceutical plant it is a turnover package that the validation team files as the equipment's permanent record, and the unit cannot go into service without it.
The organizing idea is traceability: any product-contact surface on the finished unit can be followed back to the heat of metal it was made from, the certificate for that heat, the welds that joined it, the finish reading taken on it, and the test it passed. The tools are heat numbers marked on the parts, a weld map that ties joints to heats, and reports filed against the weld map.
Mill Test Report
- Chemistry and mechanicals for one heat
- EN 10204 type 3.1 from the mill
- Heat number marked on parts before fabrication
Compliance Statement
- Compound name and the regulations met
- FDA 21 CFR 177, USP Class VI, 3-A 18-03
- Indexed into the turnover package
Documents in a sanitary exchanger package
Material and welding
- MTR (mill test report): Chemistry and mechanicals per heat; EN 10204 3.1 format
- Heat number marking: Stamped or stenciled on tube, sheets, heads and fittings before fabrication
- Weld map: Numbered joints on the drawing, each with the heats on both sides
- Weld log: Procedure, welder or machine program, date, visual result per joint
- Weld inspection: Borescope video or photos for a stated percentage of product-side welds
- Gasket compliance: Compound name, FDA 21 CFR 177, USP Class VI or 3-A 18-03 statement
Finish, test and closeout
- Surface finish report: Profilometer readings by location, instrument and cutoff
- Passivation certificate: Procedure, solution, time and temperature, verification test result
- Hydrotest report: Test pressure each side, hold time, witness, result
- Code data report: ASME U-1 or U-1A form with National Board number where stamped
- As-built drawings: General arrangement and details reflecting the shipped unit
- Turnover package (TOP): All of the above indexed, with nameplate data and spares list
Every surface traces to a heat; every heat to a cert
What each document proves
Mill test reports and heat numbers
A mill test report is the certificate the steel mill issues for one heat, a single melt of metal, listing its chemical analysis and the results of tensile, hardness and any corrosion or grain-size tests required by the material specification. EN 10204 type 3.1 is the certificate format most specifications ask for: issued by the mill's own inspection department, independent of production, and specific to the heat delivered. When tube, tubesheet plate, head material and fittings arrive at the shop, each carries its heat number, and the shop transfers that number onto the cut parts before the mill marking is lost. That transfer is what makes the rest of the traceability possible.
- Ask for 3.1 certificates for every wetted heat, including fittings and ferrules
- Check that the grade and the tube standard on the MTR match the drawing
- Keep the heat number list with the drawing so a future repair can match material
Weld maps and weld logs
A weld map is the drawing with every product-contact weld numbered. Against each number the log records the welding procedure, the welder or the orbital machine program, the heat numbers of the two parts, the date, and the inspection result. On BPE work a sample of welds, often 20 percent or more, is borescoped and the video is filed against the weld number; on 3-A work a visual of the ground and polished product side is usual. The map and log together let an auditor pick any joint on the unit and see who made it, from what, and whether it passed.
Name the documentation level on the order, not after the hydrotest.
- EN 10204 3.1 mill certificate for every wetted heat
- Borescope records on 20 percent or more of BPE welds
- Hydrotest at 1.3 times design pressure, witnessed when stamped
Finish, passivation and hydrotest reports
The surface finish report lists profilometer readings by location, with the instrument, the cutoff length and each trace, and states the acceptance limit. On a shell-and-tube unit it covers the tube bore (by heat, on sample lengths), the tubesheet product faces, the heads and the ferrule bores. The passivation certificate records the procedure, the acid, the concentration, the time and temperature, and the verification test, typically a copper sulfate or ferroxyl test, with its result. The hydrotest report gives the test pressure on each side, usually 1.3 times design pressure for ASME Division 1, the hold time, and the result, and is witnessed by the authorized inspector on a stamped unit. All three are dated and signed, and all three are routinely asked for by pharmaceutical QA and increasingly by food-plant auditors.
The turnover package for pharma
A turnover package, or TOP, is the indexed binder or electronic file that collects everything above plus the code data report, the as-built drawings, the nameplate rubbing or photo, the gasket compliance statements, and a spare parts list. Its purpose is installation qualification: the validation engineer checks the delivered unit against the package and the package against the specification, and the unit is released to service on that basis. A good TOP has a table of contents, is cross-referenced by weld number and heat number, and is delivered with the unit, not after it.
Ordering the right level
Food and beverage: MTRs for wetted metal, gasket compliance, hydrotest report, drawing. 3-A: the same plus the finish readings and the symbol authorization number. Pharmaceutical: the full turnover package with weld map, weld log, borescope records, finish and passivation reports, and code data. Name the level on the order and the package arrives with the unit.
Call and talk it through with an engineer: 1-805-484-2992
Documentation Questions
Not for product-contact metal. A certificate of conformance states that material meets a specification, with no test data on the page; a mill test report gives the measured chemistry and mechanicals for the specific heat, which is what an auditor checks against the drawing. Certificates of conformance are the right document for gaskets, fasteners and clamps, where the requirement is a formulation or a standard rather than a measured value. Order the MTR as EN 10204 3.1 for every wetted heat of tube, plate and fitting and the CoC for everything else.
Rarely on sanitary work; a 3.2 certificate adds an inspector independent of the mill who witnesses the tests and countersigns. That inspector is appointed by the purchaser or by a notified body, and the arrangement adds cost and time to the material order. It is routine on nuclear and some offshore contracts and almost unknown in food, dairy or pharmaceutical work, where a 3.1 from the mill's own inspection department is accepted. If a corporate specification says 3.2, ask whether the author meant it, because the witness has to be arranged before the mill tests the heat and cannot be added once the tube is already on the shelf.
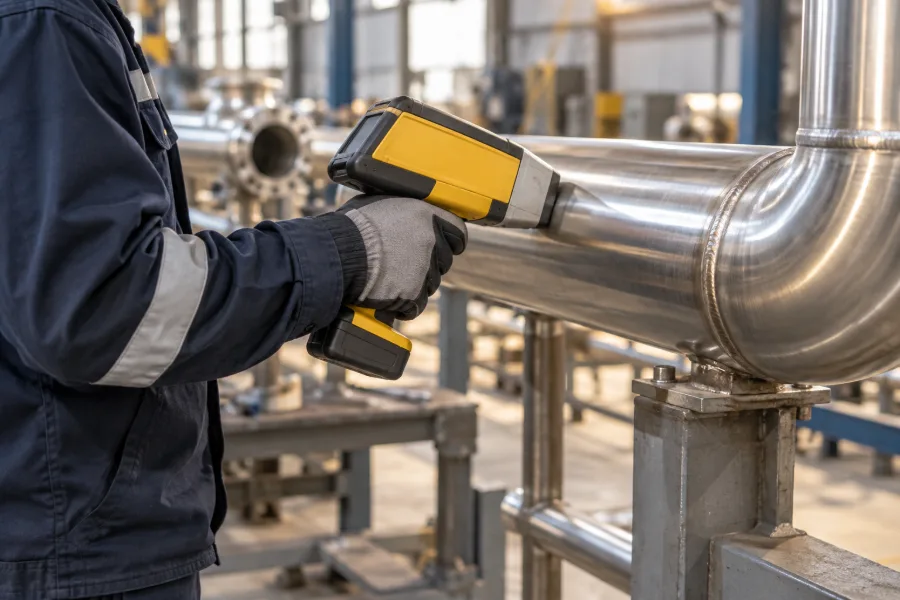
No; it supplements them. A handheld XRF reading on a finished part confirms the alloy family and the presence of molybdenum, which catches a 304L fitting that got in to a 316L build. It does not read carbon reliably and says nothing about mechanical properties, so it cannot prove an L grade or a tensile result; only the MTR does that. Pharmaceutical orders often ask for PMI on a sample of product-contact parts, recorded against the weld map, and some ask for every part. Say which on the order, and whether the readings go in the turnover package.
It becomes a nonconformance. The shop either re-identifies the part with testing the buyer accepts or scraps it and cuts a replacement from traceable stock; on a fitting or a tube length, replacement is quicker and cleaner. The real defense is transferring the heat number onto every cut piece before the mill marking is cut off, using a low-stress stamp or an approved marker.
There is no single convention, so state what you want at drawing review. An orbital tube-to-tubesheet machine can log every joint; a 200-tube straight bundle then produces 400 weld records. Most packages instead document these welds per tubesheet, with procedure, operator, heats and a visual of every joint, and reserve joint-by-joint numbering for the nozzle and head welds. A demand for individual records made after the welding is done cannot be met, so the weld map format is agreed before the first arc is struck.
Searchable electronic, bookmarked to the index, with a signed paper original only where the plant's procedures require one. Name the format, the signature method and any document numbering the plant uses on the order. A validation group that files by system and tag number will want the package indexed that way from the start. Rebuilding a package into a different structure after delivery is slow and introduces errors, and it delays the IQ the package was supposed to shorten.
Related
Design & Fabrication
304L & 316L
How to pick between the two grades, what PREN tells you, and the alloys above them for chlorides.
+ Learn More
Design & Fabrication
Gaskets & Elastomers
Which compound survives your CIP, your product and your steam, and how long before it needs changing.
+ Learn More
Design & Fabrication
Materials
The metal in the tubes, the rubber in the joints, and the paper that proves which heat went where.
+ Learn More
